
Matching Blade Velocity to Material Density for Smooth Cuts
Pushing dense metal stock through a blade running at woodcutting speed will scorch teeth and ruin expensive tooling within seconds. High surface velocity generates excessive friction against steel and cast iron, whereas lumber requires rapid chip clearance to prevent heat buildup. Determining the best sfpm for bandsaw tasks depends on stock hardness, tooth pitch, and drive capabilities. Based on a detailed comparison of motor ratings, throat capacities, and user feedback, dialing in your blade feet per minute prevents stripped teeth while keeping feed pressure steady.
Matching your blade travel rate to the material preserves motor life and dampens frame vibration. When cutting structural pipe or thick bar stock, low speeds between 100 and 250 feet per minute let teeth shear cleanly without overheating. For woodworking tasks, a vertical saw running near 2900 feet per minute yields crisp curved cuts that need minimal smoothing on an oscillator sander for woodworking and detail sanding at the workbench. Our research into the listed manufacturer features suggests that rigid guide setups and correct blade speed guarantee reliable shop performance.

Frequently Asked Questions
What is the best sfpm for bandsaw cutting in carbon steel and iron?
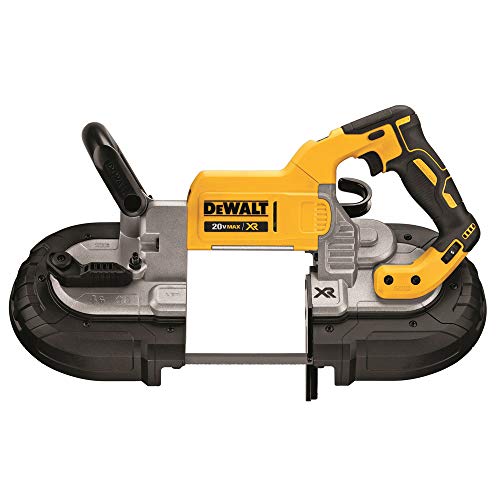
Between 100 and 250 SFPM is optimal for cutting ferrous metals like structural steel. Operating at higher velocities creates extreme friction that softens teeth tips and strips a bimetal blade. Dedicated hydraulic bandsaws running between 100 and 256 SFPM allow teeth to shear dense metal cleanly without work-hardening the workpiece.
What blade speed is recommended for woodworking and curved cuts?
Speeds between 2,500 and 3,500 SFPM deliver the cleanest results in natural lumber. High blade speed clears wood shavings quickly before gullets pack with dust. Operating near 2,900 SFPM produces silky edges on hardwoods, which saves time when smoothing curves with a detailing sander for tight spaces during final assembly.
Can you cut steel on a standard vertical woodworking bandsaw?
No, standard woodworking bandsaws run far too fast to cut ferrous metals safely. Wood saws operate at roughly 2,500 to 3,000 SFPM, which will instantly dull or shatter teeth against steel. Cutting dense metal requires a gearbox reduction or hydraulic saw running below 300 SFPM.
How does blade tooth pitch interact with surface feet per minute?
Coarser tooth counts require rapid speeds in wood, while fine pitch demands low speed in metal. Resawing thick timber at high SFPM requires 3 to 4 TPI for gullet clearance without stalling the motor. Metal cutting uses 10 to 18 TPI at low velocity to ensure continuous tooth engagement.
Does improper blade velocity cause blade drift during rip cuts in 2026?
Yes, excessive blade speed causes teeth to skate and deflect against guide blocks. When teeth cannot bite cleanly, feed pressure forces the blade off your layout line. Using the best sfpm for bandsaw operations keeps tracking stable against the rip fence.






Write Your Review
No reviews yet. Be the first to share your experience!